Warehouse Floor Design and Racking
Warehouse floor design should start from the racking and handling equipment that will run on it, not from a generic industrial slab. Point loads under racking legs, wheel loads from forklifts, floor flatness for the truck type, and the joint layout all depend on equipment data that must be fixed before the slab is cast.
By Dhruv Agarwal · · 7 min read
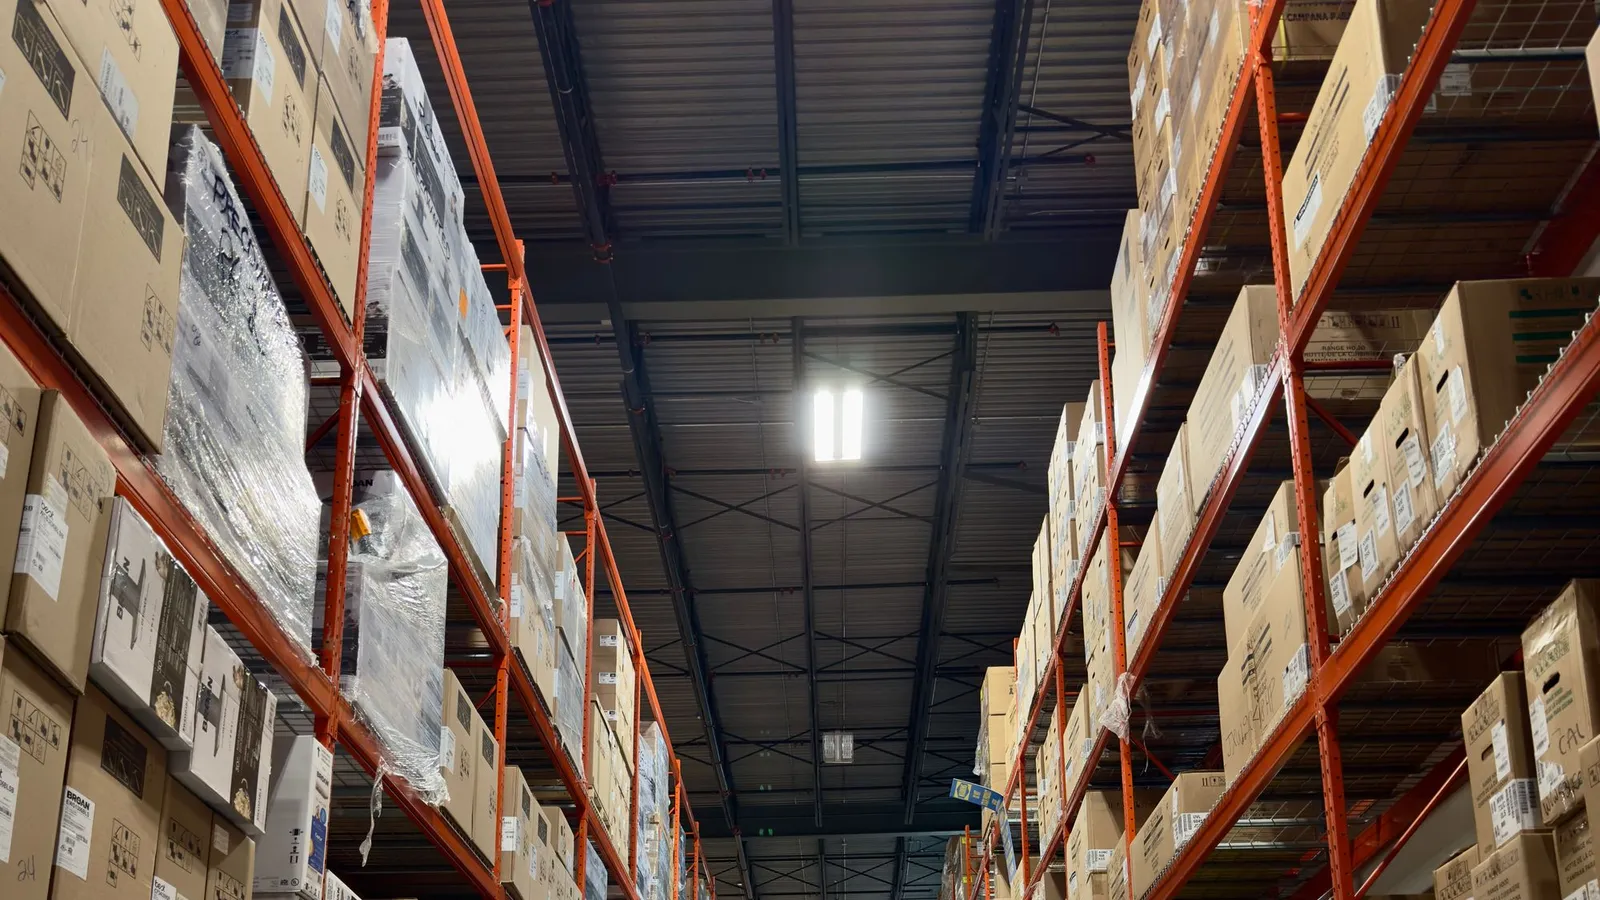
Warehouse floor design: built first, judged last
A warehouse slab is one of the earliest large pours on the job. The racking, the trucks and the storage system that will sit on it are usually chosen much later, often by a different team, sometimes after the building is otherwise complete.
That order is the problem. The floor is designed against assumptions, and the equipment later turns out to have different requirements. By then the concrete is cured, and changing it means grinding, cutting and re-laying, in a building that is meant to be earning money.
For a CEO or CFO the decision is simple to state: the floor is a piece of equipment for the operation, and it should be specified from the equipment's data. For the facilities head, it means asking for that data before the slab drawings are frozen, not after.
What the floor actually has to carry
A warehouse floor sees two different kinds of demand, and they are designed for separately.
| Demand | Where it comes from | Why it matters |
|---|---|---|
| Distributed load | Pallets on the floor, block stacking, general storage | Spread over an area; usually the easier case |
| Point load | Base plates of racking uprights | Concentrated on a small footprint; a different design problem |
| Wheel load | Forklifts, reach trucks, pallet movers | Repeated, moving, and often on small hard wheels |
| Joint crossing | Any truck crossing a joint | Damages joint edges over time |
The same total weight can be comfortable when spread out and demanding when concentrated under a few upright feet. That is why the structural engineer needs the racking supplier's actual base reactions and the truck's actual wheel data, not simply a number for tonnes stored. Those figures are set for each project by the engineer. This article does not, and should not, give them.
Racking design itself is governed by its own standard, such as EN 15512 for adjustable pallet racking, and the racking supplier is responsible for that side. The floor engineer needs what comes out of it.
Flatness depends on the truck, not the building
There is a persistent belief that a warehouse floor should simply be "as flat as possible". Flatness costs money and depends heavily on the method, so it is worth being specific about what it is for.
Trucks running in wide aisles and lifting to modest heights tolerate more variation than trucks running in a very narrow aisle. Very narrow aisle equipment lifts to height in a guided or fixed track, and small variations in the floor become large movements at the top of the mast. For that equipment the truck manufacturer states a floor tolerance and often the measurement method to be used.
The practical consequences:
- The tolerance is a requirement of the equipment, so it comes from the equipment supplier, not from a generic specification.
- The floor contractor must be able to demonstrate it can deliver that tolerance with their method and equipment, before the pour.
- Aisles where tight tolerance is needed and areas where it is not can be treated differently, rather than paying for the highest requirement across the whole floor.
Tolerance classes and measurement methods are published in documents such as DIN 15185 for very narrow aisle areas and in slab guidance such as ACI 360R. The tolerance that applies to a specific truck is the truck supplier's to state.
Joints are where traffic and racking collide
A large concrete slab shrinks as it cures and dries, and it cracks unless the movement is controlled with joints. The joint layout is therefore not optional; the design question is where the joints fall relative to the racking and the traffic.
Three things to check on the layout drawing:
- Joints running across main truck routes. Every crossing is a repeated impact on the joint edge. Hard, small wheels are the harshest case.
- Joints passing under racking uprights. A joint below a base plate can mean a load bearing on an edge or on two panels moving differently.
- Joint edge protection and filler. Edges that are unprotected or filled with the wrong material chip, and a chipped joint becomes a bump that trucks and loads feel every time.
Because the storage layout and racking lines are not usually known when the slab is first drawn, the joint layout is often set by construction convenience. That is the moment to ask for the racking plan, even a draft one, so joints and routes can be arranged against each other. Where a joint layout cannot be changed, the routes or racking lines may be able to.
Curing and shrinkage are part of the design
How a slab is cured affects its strength, its surface and how much it cracks. Concrete gains strength through a chemical reaction that needs moisture and time, and a large surface area dries quickly. Poor curing shows up later as surface dusting, cracking and curling at edges and joints, which then affect flatness.
The programme pressure on a warehouse is real, but the floor is one place where taking time out of curing costs more than it saves, because the defect appears after handover and in a working building. See our note on concrete curing for how it works. The engineer and the concrete supplier set the mix, the reinforcement approach and the curing regime, following the concrete code, IS 456, and the project specification.
Surface treatment is a separate decision from the slab
The surface finish of the slab and the treatment applied to it are different things. A hardened, dust-proofed concrete surface, a sealer, a coating or a topping each behave differently under wheel wear, chemical spills and cleaning.
Which suits a warehouse depends on the traffic, the cleaning regime, the products stored and how much downtime the operation can tolerate during application. Our comparison of epoxy and vinyl industrial flooring sets out how the main options differ. One point is worth stating early: most surface treatments depend on the slab being sound and adequately cured, so they cannot be used to rescue a slab that was poured to the wrong tolerance.
The sequence problem
The chain of decisions usually runs like this: the building shell is procured, the slab is designed and cast, and then the racking, trucks and storage layout are selected. The floor has already committed to the wrong things, or to nothing in particular.
The way out is to bring forward three decisions:
- A draft storage and racking layout, even if the supplier is not yet fixed.
- The class of handling equipment, because that sets the tolerance and wheel demands.
- A responsible person who collects supplier data and passes it to the structural engineer before the slab drawings are released.
The building choice matters here too. Steel structures and reinforced concrete structures handle floor loads and construction sequence differently, and our comparison of PEB and RCC industrial buildings covers the wider decision, including the tapered-frame PEB approach. The floor still needs the same equipment data whichever structure is chosen.
Common mistakes
- Designing to tonnes stored, rather than to racking base reactions and truck wheel data.
- Specifying the tightest flatness everywhere, when it is needed only in certain aisles, or specifying it without checking the contractor can build it.
- Setting joints by convenience, then discovering they cross the main truck route.
- Shortening the curing to hold a handover date.
- Choosing the racking after the pour and assuming the floor will suit it.
- Treating the coating as a fix for a slab that was not built to the right tolerance.
What to ask
- Do we have the racking supplier's base reactions and the equipment supplier's wheel data, and has the structural engineer used them?
- Which aisles need the tightest tolerance, and can the floor contractor show they can achieve it?
- Where do joints fall against the truck routes and the racking lines?
- How is joint edge protection being handled?
- What curing regime is specified, and is it protected in the programme?
- What surface treatment is intended, and does it suit the slab as built?
Standards referenced
Concrete design and construction under IS 456; racking structural design principles under EN 15512; guidance on slab-on-ground design and tolerances in ACI 360R; and floor tolerances for very narrow aisle areas in DIN 15185. The loads, tolerances, thicknesses, joint layout and reinforcement for a specific project must be set by the project's structural engineer from the actual racking and equipment data.
Standards referenced
- IS 456 — Plain and reinforced concrete - code of practice
- EN 15512 — Steel static storage systems - adjustable pallet racking - principles for structural design
- ACI 360R — Guide to design of slabs-on-ground